

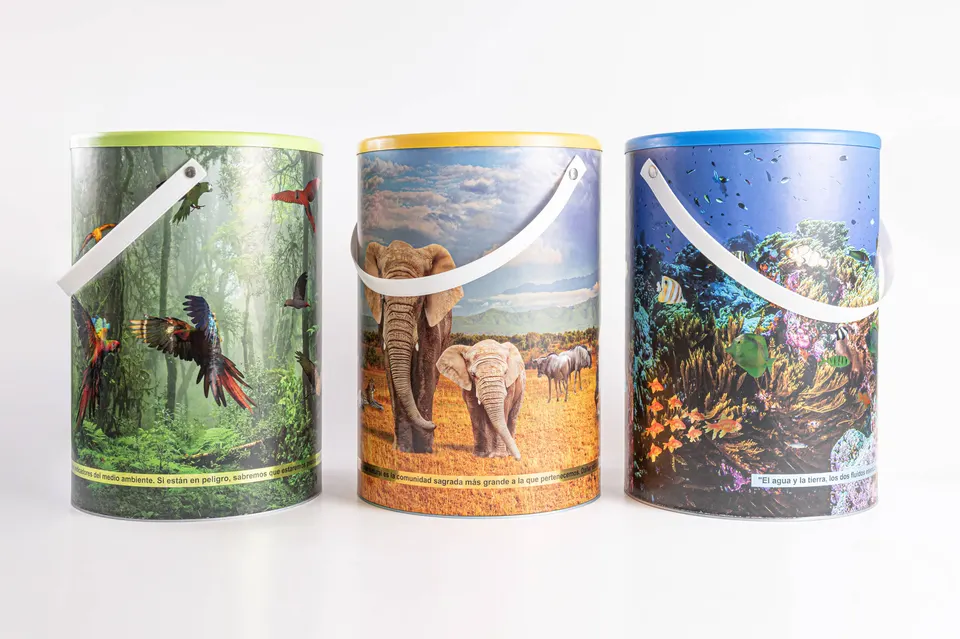
In highly regulated sectors such as the pharmaceutical, chemical and food industries, choosing the right packaging is a key factor in ensuring safety, hygiene and efficiency in the storage and transport of products. Laminated cardboard drums, made with folding board laminated on both sides, have established themselves as one of the most versatile and effective options. Below, we look at their advantages and why they are the best choice for these industries.
1. Maximum safety and hygiene
One of the main benefits of laminated cardboard drums is their ability to provide a safe, hygienic environment for the products stored. Their innovative design offers:
- Laminated surface on both sides: this prevents moisture absorption and minimises the risk of contamination.
- High chemical resistance: the material used is compatible with sensitive products and avoids unwanted reactions.
- Rolled-edge lid in the same material: provides an airtight seal that prevents leaks and maintains the integrity of the contents.
2. Strength and durability
Laminated cardboard drums are designed to withstand demanding conditions, offering:
- Robust, reinforced structure: able to resist impacts and pressure during transport and storage.
- Protection against external agents: their laminated surface protects against moisture, dust and other contaminants.
- Lightness without compromising strength: unlike metal or rigid plastic containers, laminated cardboard drums are lighter, making them easier to handle and reducing transport costs.
3. Sustainability and environmental commitment
More and more industries are looking for packaging alternatives that reduce their environmental impact without compromising quality. Laminated cardboard drums offer significant advantages in this respect:
- Recyclable material: unlike conventional plastic, laminated cardboard can be recycled with the right processes, reducing the ecological footprint.
- Lower energy consumption in manufacture: their production requires fewer resources than metal or plastic drums.
- Compliance with environmental regulations: their design and materials allow them to meet international ecological regulations.
4. Versatility for different sectors
These drums are specially designed to meet the specific needs of the pharmaceutical, chemical and food industries:
Pharmaceutical industry
- Safe storage of active ingredients and excipients.
- Protection against contamination and moisture.
- Compliance with strict safety regulations.
Chemical industry
- Ability to contain sensitive substances without risk of leakage.
- Resistance to aggressive products.
- Easy handling and safe storage.
Food industry
- Suitable for dry and powdered ingredients.
- Hygienic, easy-to-clean surface.
- Preservation of product quality.
If you are looking for reliable, efficient packaging for your company, at FATECSA we offer the best solutions in laminated cardboard drums. Get in touch and find out how we can help you optimise your logistics and storage with high-quality products. You can get advice and a quote on our website www.fatecsa.com
You can also follow us on our LinkedIn page to catch our latest news.